
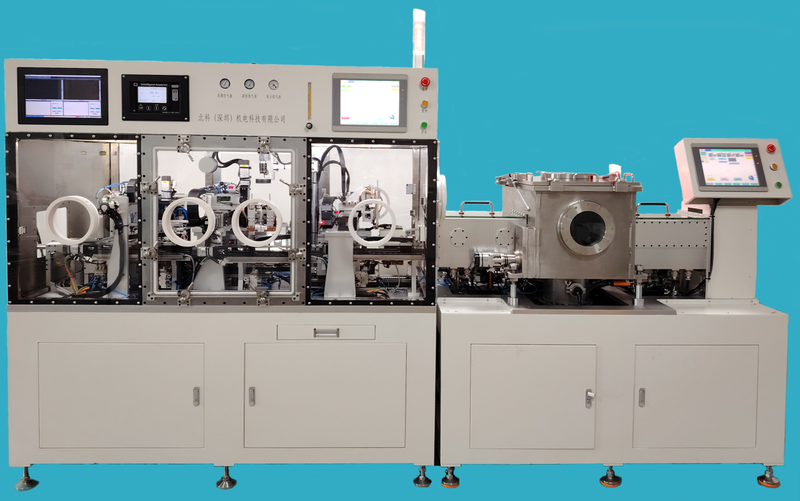
FIS-2010VB Fully Automatic Vision-Guided Vacuum/Backfill Parallel Seam Welder
This equipment hermetically seals large rectangular, optoelectronic and flat metal packages. Base trays are loaded into fixtures and dried in an upstream automatic oven, then transferred to the working platform. A robot moves the base fixture to the tack-weld position. Covers loaded into magazines undergo trace-moisture removal and enter the welding chamber via a track. The operator places them manually into the positioning mechanism. Package and base CCD vision systems capture geometry and use algorithms to adjust angle, align data and fit the parts precisely for tack welding. Automatic rolling seam welding seals X and Y edges inside a closed nitrogen glovebox. For high-vacuum products, after all long X edges are welded, packages transfer automatically to a high-vacuum welder for evacuation and special-gas backfilling, then short Y edges are sealed and products transfer to collection.
 Save to Favorites
Overview
Specifications
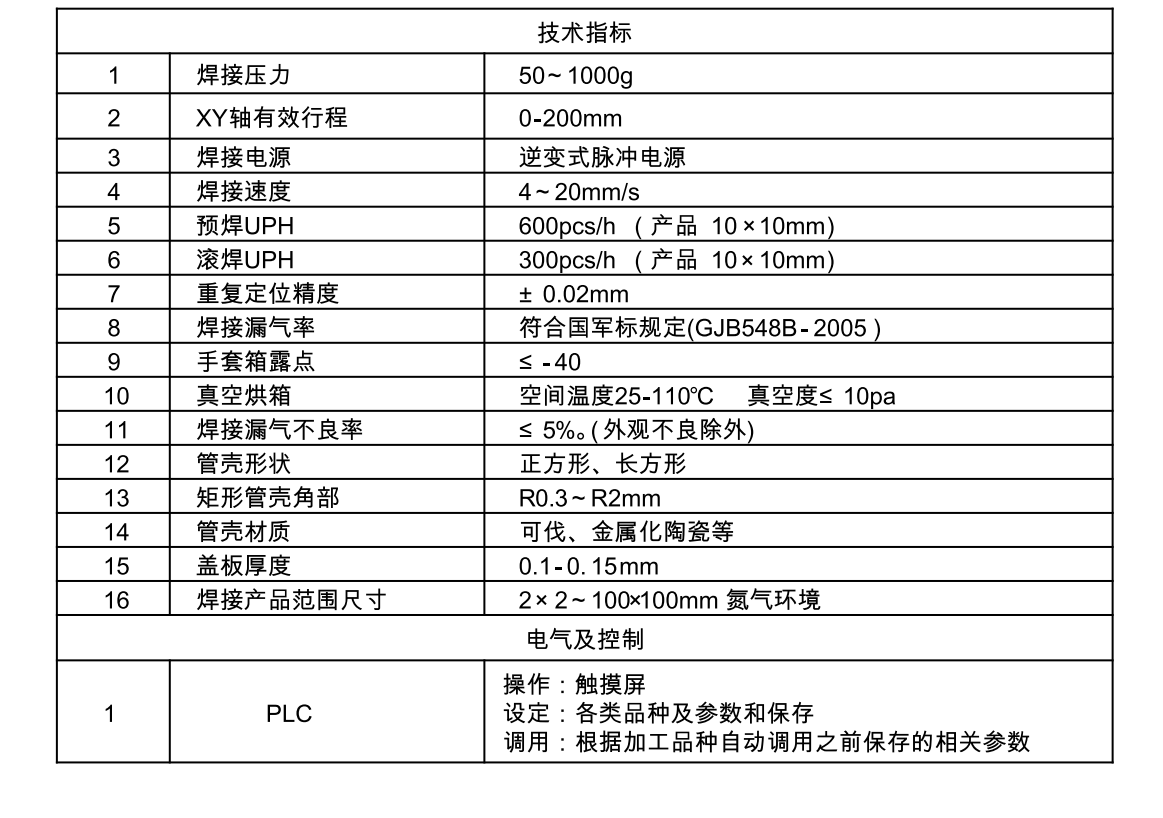
| Parameter | Value |
|---|---|
| Welding Pressure | 50~1000g |
| XY-Axis Effective Travel | 0-200mm |
| Welding Power supply | Inverter-Type Pulsed Power Supply |
| Welding Speed | 4~20mm/s |
| Prewelding UPH [Product 10×10mm] | 600pcs/h |
| Roll-Welding UPH [Product 10×10mm] | 300pcs/h |
| Positioning Repeatability | ±0.02mm |
| Weld Gas-Leak Rate | Complies with the military standard GJB548B-2005 |
| Glovebox Dew Point | ≤-40 |
| Vacuum Oven-Chamber Temperature | 25-110℃ |
| Vacuum Oven-Vacuum | ≤10pa |
| Weld Gas-Leak Defect Rate [Excluding Cosmetic Defects] | ≤5‰ |
| Package Shape | Square, Rectangle |
| Rectangular Package Corner | R0.3~R2mm |
| Package Material | Kovar, metallized ceramics, etc. |
| Cover Plate Thickness | 0.1-0.15mm |
| Welding Workpiece Size Range [Nitrogen Atmosphere] | 2×2~100×100mm |
Applications
Datasheet
Please provide your email to download the datasheet.
Invalid email format. Please try again.
Supplier Information
Related Products
-
 AMB/DBC Substrate CO2 Laser Scribing Machine CPP12
Semiconductor Packaging Equipment
Delphilaser
Equipment Type: Single Head, Single Platform, Standalone/Automated Working area: 200mm×200mm(customizable) Positioning accuracy: ±3μm
This equipment is mainly used for laser scribing in the DBC industry and is widely used in packaging fields such as power electronic modules, semiconductor cooling and LED devices.
-
 AMB/DBC Substrate CO2 Laser Scribing Machine CPP21
Semiconductor Packaging Equipment
Delphilaser
Equipment Type: Dual Heads, Dual Platforms, Automated Working area: 200mm×200mm(customizable) Positioning accuracy: ±3μm
This equipment is mainly used for laser scribing in the DBC industry and is widely used in packaging fields such as power electronic modules, semiconductor cooling and LED devices.
-
 AMB/DBC Substrate CO2 Laser Scribing Machine CPP30
Semiconductor Packaging Equipment
Delphilaser
Equipment Type: Single Head, Single Platform, Automated Working area: 200mm×200mm(customizable) Positioning accuracy: ±3μm
This equipment is mainly used for laser scribing in the DBC industry and is widely used in packaging fields such as power electronic modules, semiconductor cooling and LED devices.
-
 Compact Air-Cooled Nanosecond Laser All-in-One Unit Coral-A Series Coral UV-A
Semiconductor Packaging Equipment
Bellinlaser
Spot Mode: TEM₀₀(M²<1.3) Beam diameter: 0.5-1mm Power stability [RMS over 8 hours]: <3% RMS over 8 hours
-
 Compact Air-Cooled Nanosecond Laser All-in-One Unit Coral-A Series Coral GR-A
Semiconductor Packaging Equipment
Bellinlaser
Spot Mode: TEM₀₀(M²<1.3) Beam diameter: 0.5-1mm Power stability [RMS over 8 hours]: <3% RMS over 8 hours
Related Articles
Electro-optic deflectors (EODs) are optical devices used to steer or deflect light beams by applying an electric field to a specialized optical crystal. Unlike mechanical beam steering systems that rely on moving mirrors, electro-optic deflectors enable high-speed, non-mechanical beam control with exceptional precision and responsiveness. They are widely used in laser scanning, optical communications, microscopy, laser printing, spectroscopy, and scientific research, where rapid and accurate laser beam positioning is essential.
The 850 nm and 940 nm infrared narrow‑bandpass filters launched by Innovation Photoelectric are core optical components specially designed for day‑and‑night security cameras. They effectively eliminate image interference during visible‑light and infrared‑illumination switching, delivering stable round‑the‑clock monitoring performance.
Within cutting‑edge ultrafast photonics research, asynchronous optical sampling (ASOPS) and synchronous sampling serve as fundamental technologies for terahertz excitation detection, coherent Raman imaging and other time‑resolved spectroscopy experiments.
Shanghai Connet Laser Technology Co., Ltd. focuses on technological innovation, delivering cutting-edge photonic products & solutions for industrial lasers, LiDAR, fiber optic sensing, coherent telecom, cold atom physics and precision spectroscopy research & mass manufacturing.
Loading...
Name
Phone
Organization
Use Case

Database Platform