
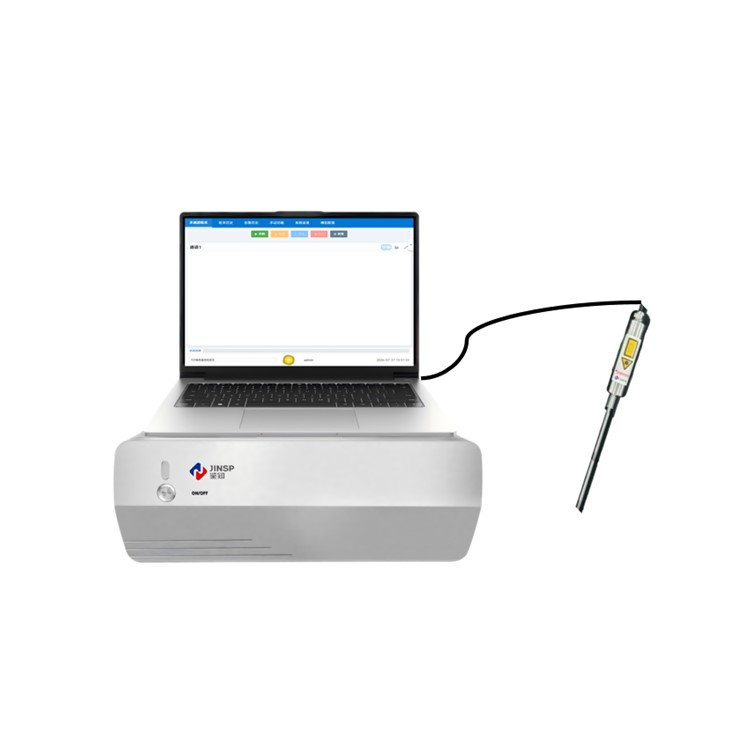
Inline Raman analyzer RS2000 Series
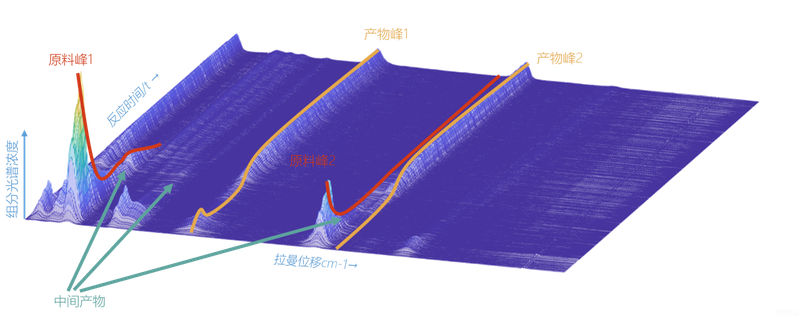
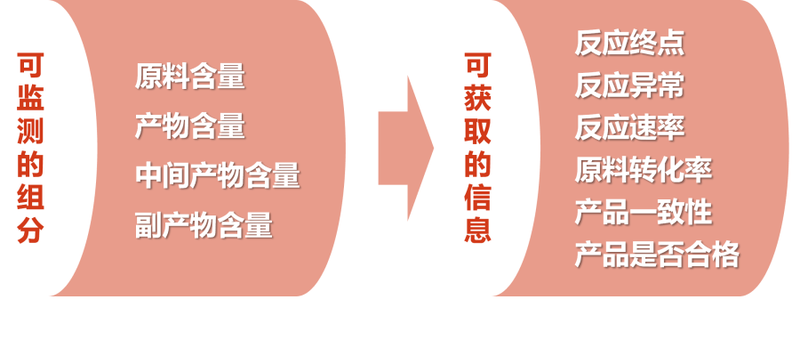
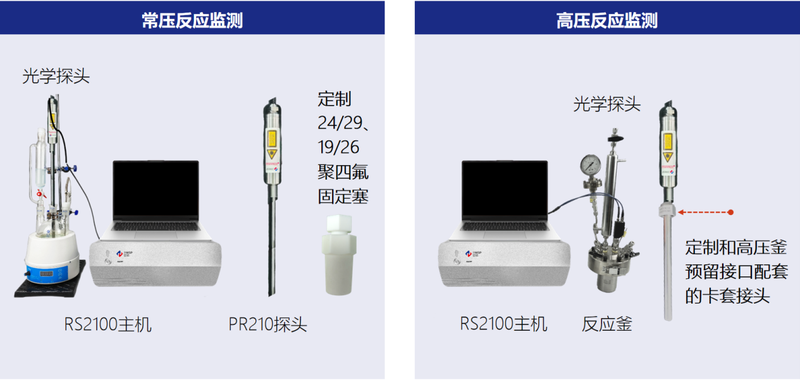
Chemical, pharmaceutical and materials process development and production require qualitative and quantitative composition analysis. Conventional offline laboratory analysis uses chromatography, mass spectrometry and nuclear magnetic resonance after sample collection to determine component concentrations. Long testing times and low sampling frequency cannot meet real-time monitoring requirements. Jianzhi Technology provides online monitoring solutions for chemical, pharmaceutical and materials process development, enabling in-situ, real-time, continuous, rapid monitoring of reaction-component concentrations. Particularly suitable for hazardous reactions such as nitration, chlorination, fluorination, hydrogenation and diazotization, RS2000/RS2100 online Raman analyzers track raw materials, products and intermediates in real time to help researchers understand reaction progress and mechanisms. They flexibly accommodate atmospheric- and high-pressure reactors.
 Save to Favorites
Overview
Specifications
| Parameter | Value |
|---|---|
| Excitation wavelength | 785nm |
| Number of detection channels | 1, Single channel |
| Main unit dimensions | 496 mm (length) × 312 mm (width) × 185 mm (height) |
| Main unit weight | No more than 10 kg |
| Probe | Supplied as standard with 1 each of a non-immersion fiber probe and an immersion probe; other probe models or flow cells optional |
| Communication Interface | USB 2.0, Expandable RS485 |
| Communication Protocol | Modbus |
| Spectral data output format | Selectable csv, txt, and other formats |
| Power supply | 100 ~ 240 VAC,50 ~ 60 Hz |
| Operating Temperature | 0 ~ 40 ℃ |
| Storage temperature | -20 ~ 55 ℃ |
| Relative humidity | 0~90%RH |
| Equipment power | 50 W |
| Warm-up time | <5 min |
Applications
Key Features
Datasheet
Supplier Information
Related Products
-
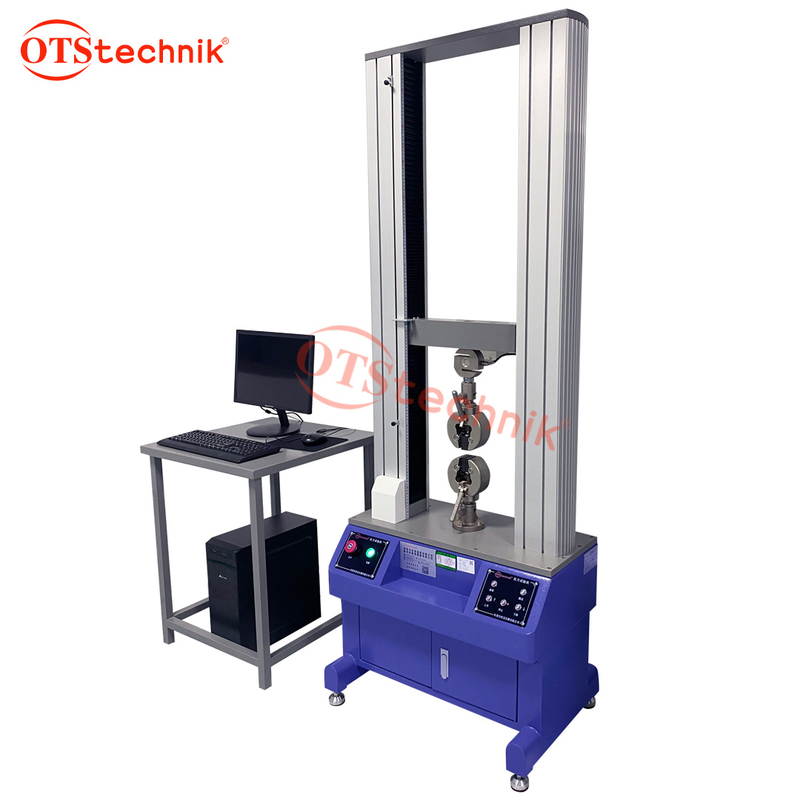 Universal Material Tensile Test Machine XB-OTS-kg
Material Analysis and Forensics
Otschina
Maximum Test Force [One range is included as standard; up to three additional ranges can be selected.]: 5N, 10N, 20N, 30N, 50N, 100N, 200N, 300N, 500N, 1KN, 2KN, 3KN, 5KN, 10KN, 20KN, 30KN and 50KN. One range is included as standard, with up to three additional ranges optional. Accuracy Grade: Class 0.5/Class 0.25 Test Force Measurement Range [Full scale]: 0.2%~100%FS( Full scale )
Prints multiple data sets and generates comparative graphs. Modular design and comprehensive accessories provide flexible configurations. It performs cyclic constant-stress, constant-strain, creep, relaxation, axial and radial tests. Under GB, JIS, ASTM and DIN standards, it calculates tensile strength, yield strength, elongation, stress at specified elongation, elongation at specified stress, elastic modulus, elongation at break, peel strength including 90°/180° peeling, flexural modulus, breaking strength, bond strength and shear strength.
-
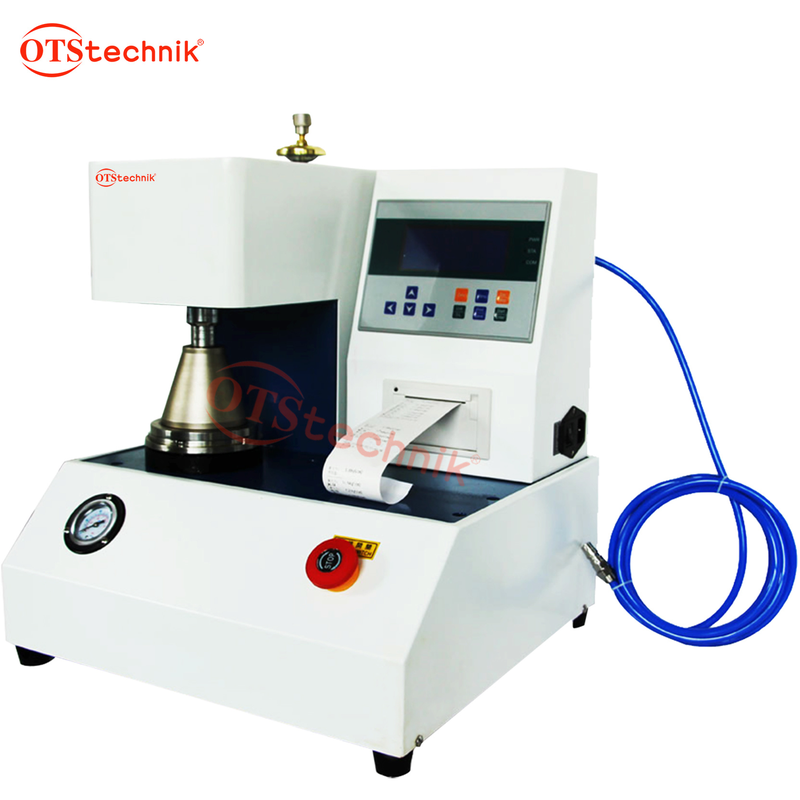 Fully Automatic Carton Burst-Strength Test Machine XB-OTS-209A
Material Analysis and Forensics
Otschina
Dimensions: 43x35x58(WxDxH)cm Capacity: 0-5KG/cm2 Hydraulic oil: Glycerol 85%, Distilled Water 15%
After material loading, the instrument automatically detects and tests the specimen, returns hydraulic pressure and calculates, stores and prints results. Hydraulic pressure ramping, microcomputer detection/control and digital signal processing measure bursting strength in accordance with ISO2759 and GB/T1539 paperboard bursting-strength test standards.
-
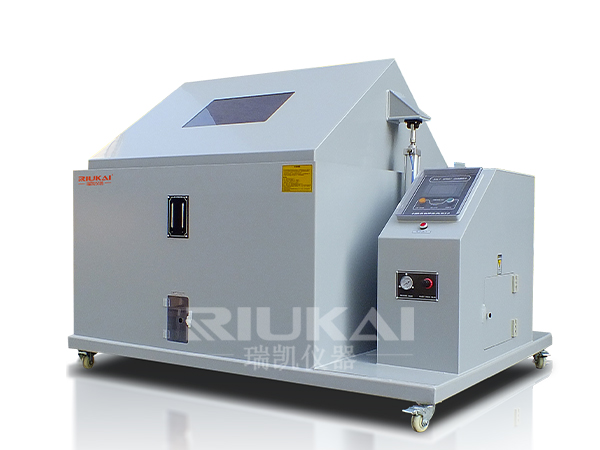 Salt Spray Test Chamber R-YW-90
Material Analysis and Forensics
Riukai
Working Chamber Dimensions D×W×H: 600 mm × 900 mm × 500 mm Overall dimensions (HxWxD): 770×1450×1200 Power: 3.0(kw)
The salt-spray corrosion test chamber evaluates sample corrosion resistance by testing materials and protective coatings under salt spray. It compares the process quality of similar protective coatings and evaluates the salt-spray resistance of certain products.
-
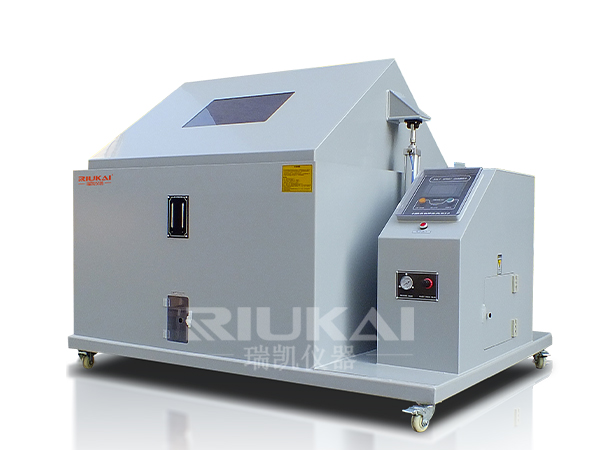 Salt Spray Test Chamber R-YW-120
Material Analysis and Forensics
Riukai
Working Chamber Dimensions D×W×H: 750 mm × 1100 mm × 500 mm Overall dimensions (HxWxD): 920×1650×1450 Power: 3.0(kw)
The salt-spray corrosion test chamber evaluates sample corrosion resistance by testing materials and protective coatings under salt spray. It compares the process quality of similar protective coatings and evaluates the salt-spray resistance of certain products.
-
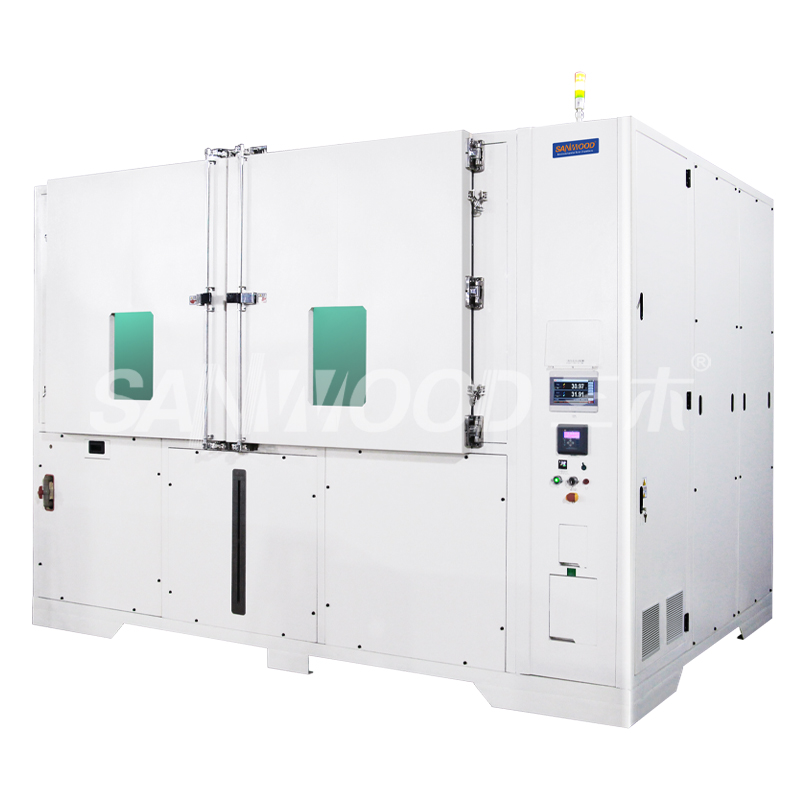 Integrated Saltwater Test Bath
Material Analysis and Forensics
Sanmutest
Test Standards Met: JB/T5376 technical requirements for low-temperature constant-temperature baths; GB/T 2423.2-2008 test B high-temperature method; GJB 150.3A-2009 B high-temperature test; JB / T5520-91 technical requirements for drying ovens. Overall Dimensions: 4350x2650x3100mm(W*H*D) Saltwater Tank Interior Dimensions: 3150x2200x900mm(W*H*D)
The salt-spray chamber is used in aerospace, aviation, electronics, automotive and battery industries to test corrosion of electrical/electronic products, metals, parts and equipment. Tests evaluate materials and protective coatings under specified conditions. The humidity/temperature salt-spray tester supplier tests corrosion resistance under severe environmental changes for automotive and aviation equipment, photographic equipment, building materials, power, electrical and electronic systems.
Related Articles
In photonics and laser technology, devices that manipulate optical signals via the electro-optic effect form the backbone of precision optical systems. Electro-optic phase modulators and electro-optic deflectors are two prominent examples of this device category. As a critical hardware solution for high-speed, high-accuracy laser beam direction control, electro-optic deflectors are widely deployed across industrial and research settings. Below is a detailed overview of their core structure, key performance drivers, and primary use cases.
As a top‑tier supplier of tunable laser chips, Shandong Zhongxin Optoelectronics Technology Company has newly launched the world’s first budget‑friendly fiber‑Bragg‑grating (FBG) demodulator and scanning module.
A laser bar is an array semiconductor laser chip integrated with dozens of emitters, which realizes hundred-watt quasi-continuous output on a single chip. With regular emitter arrangement and controllable fill factor, integrated thermal design and superior wall-plug efficiency compared to single chips, it acts as the core light source for high-power pumping, medical lasers and precision processing.
BEIJING JIEPU TREND supplies YAG+Er:YAG+YAG bonded composite slab laser crystals for high‑power solid‑state laser systems. The monolithic slab consists of two undoped YAG end‑cap layers and a central Er‑doped YAG gain segment. The overall dimension is 9 mm×9 mm×9 mm.
Loading...
Name
Phone
Organization
Use Case

Database Platform